About Sorbic Acid
We are a specialized company in innovation, production, and distribution of agricultural chemicals, industrial chemicals, food chemicals, inorganic chemicals, mining chemicals and organic chemicals
1. 100+ food/feed ingredients. 2. 138 food ingredients formulas. 3. 5 invested factories to ensure excellent quality and stable supply. 4. 2 labs with 30 technicians to provide formulas and technical support. 5. 5 warehouses covering an area of 5,000 square meters to ensure competitive prices.
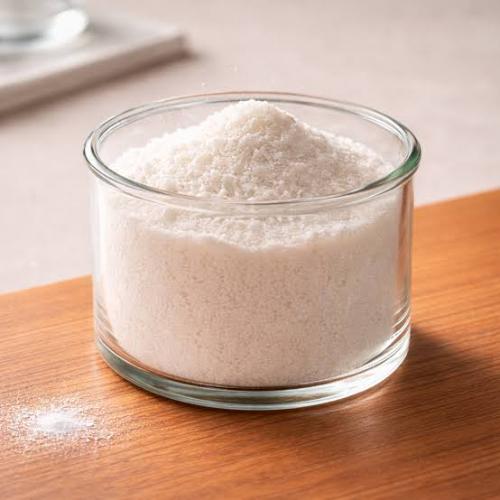
Effective Preservation Across IndustriesSorbic Acid is renowned for its antimicrobial properties, making it a preferred preservative in the food, pharmaceutical, and cosmetic sectors. By inhibiting the growth of yeast and molds, it effectively extends the freshness and shelf life of products without compromising safety or quality. Its widely recognized safety profile (GRAS) underscores its suitability for large-scale applications.
Reliable Quality and Versatile SolubilityOffered at high purity (99.0%) and low moisture content, Sorbic Acid meets stringent quality standards. Its compatibility with various solvents ensures easy integration into a broad range of formulations. Whether you need a food-grade or industrial solution, its storage stability and adaptability make it an excellent choice for businesses worldwide.
FAQ's of Sorbic Acid:
Q: How should Sorbic Acid be stored to maintain optimal quality?
A: Sorbic Acid should be stored in a cool, dry, and well-ventilated space. Keeping it in its original, unopened packaging will help maintain its stability and efficacy for up to 24 months.
Q: What is the main benefit of using Sorbic Acid in food and other products?
A: The primary benefit of Sorbic Acid is its effectiveness as a preservative, inhibiting the growth of molds and yeasts. This extends shelf life and maintains product safety and quality in foods, pharmaceuticals, and cosmetics.
Q: Where is Sorbic Acid typically used?
A: Sorbic Acid is commonly used in the food industry (for bakery products, cheeses, and beverages), as well as in pharmaceuticals and cosmetic formulations, to prevent spoilage caused by microorganisms.
Q: What is the process for incorporating Sorbic Acid into products?
A: Sorbic Acid is often dissolved in ethanol or an appropriate organic solvent, given its slight solubility in water, before blending with the final product. Precise amounts are used to meet preservation requirements and comply with regulatory standards.
Q: What grades of Sorbic Acid are available and how do they differ?
A: Sorbic Acid is available in food grade and industrial grade. Food grade is used for consumable products and meets stricter safety standards, while industrial grade may be used in non-food applications such as packaging or technical products.
Q: How is Sorbic Acid packaged and shipped?
A: Typically, Sorbic Acid is supplied in 25kg drums or bags. Packaging can be customized based on customer requirements, ensuring convenient handling and transport while preserving product integrity.




 Send Inquiry


 Send Inquiry
 Send Inquiry
