About Ethyl Alcohol
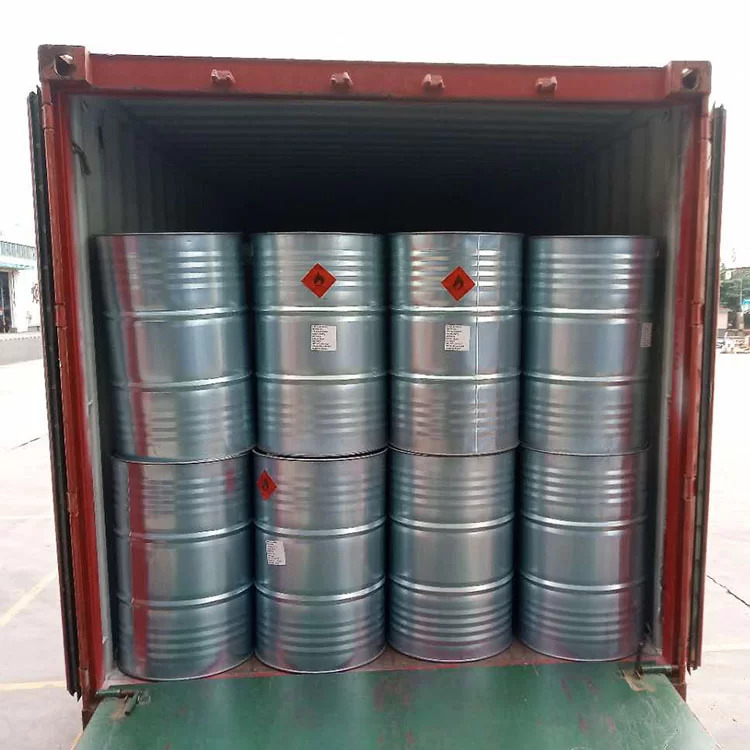
Find the distinguished Ethyl Alcohol-an opulent solution famed for its clarity and purity (minimum 99%). Securely shipped in bulk 200-liter metal drums, this highly flammable, clear, colorless liquid (UN Number: 1170) meets rigorous ASTM/ISO standards, making it ideal for industrial, laboratory, and medical applications. Its renowned miscibility with water and burning taste exemplify its versatility, while its famed neutral pH and non-toxic nature (except in excess) promise superior safety. Instantly Add to Cart and enjoy instantaneous checkout-the preferred choice of South African exporters, suppliers, and traders.
Wide-Ranging Applications of Ethyl Alcohol
Ethyl Alcohol (Ethanol) is ideal for use as a solvent, disinfectant, and laboratory reagent. Its opulent versatility extends to the medical sector, pharmaceutical preparations, surface sanitization, and industrial processes. It finds famed application in laboratories, hospitals, and industrial plants. Ethanol's adaptability grants it essential status where purity and reliability are required, making it a preferred choice for numerous industries demanding impeccable results every time.
Export Markets, Sample Policy & Certifications
Estimate the global reach of Ethyl Alcohol as it is shipped to key international export markets from South Africa. Shipped goods are managed under a robust sample policy, allowing buyers to assess quality before committing. Certified under ASTM/ISO standards, Ethyl Alcohol assures both seamless transportation and trusted performance. Exporters and traders are assured of consistent, distinguished quality with every shipment, meeting the expectations of discerning global clientele.
FAQ's of Ethyl Alcohol:
Q: How is Ethyl Alcohol commonly transported for bulk orders?
A: Ethyl Alcohol is shipped in bulk using robust 200-liter metal drum containers, ensuring safe and efficient transportation, especially for industrial and laboratory use.
Q: What are the primary sites of application for Ethyl Alcohol?
A: Ethyl Alcohol is highly valued in laboratories, medical facilities, industrial plants, and pharmaceutical manufacturing due to its purity, solvent capabilities, and disinfectant properties.
Q: What is the process for ensuring the quality and standard of Ethyl Alcohol?
A: Each batch of Ethyl Alcohol is produced to meet ASTM/ISO standards, ensuring consistent quality and performance. Samples can be provided for quality assessment prior to shipment.
Q: When should Ethyl Alcohol be stored and handled with caution?
A: Due to its high flammability (flash point: 13C), Ethyl Alcohol should always be stored in tightly closed containers in cool, well-ventilated areas and kept away from ignition sources.
Q: What are the major benefits of using Ethyl Alcohol in industrial and laboratory settings?
A: The main benefits include its high purity, excellent solvency, rapid evaporation, non-toxicity (under controlled use), and versatility in a wide range of applications from disinfection to chemical synthesis.




 Send Inquiry


 Send Inquiry
 Send Inquiry
